Price questions about these machines rarely fail for lack of numbers; they fail because the numbers arrive without the configuration attached. A $3,000 machine and an $11,000 machine are both honestly called CNC wood lathes, and the gap between them is entirely explainable. This guide attaches the explanation, walks the bands in order, prices the costs the invoice leaves out, and finishes with the payback arithmetic, so the band that matches your catalog and volume identifies itself by the end.
One more framing note before the numbers. These bands compress weeks of scattered marketplace research into a single table, but they describe configuration tiers rather than fixed quotes. Freight, voltage options, blade packages, and feeder add-ons move any individual machine within its band, so treat the band as the neighborhood and the itemized quote as the address.
What Actually Sets the Price
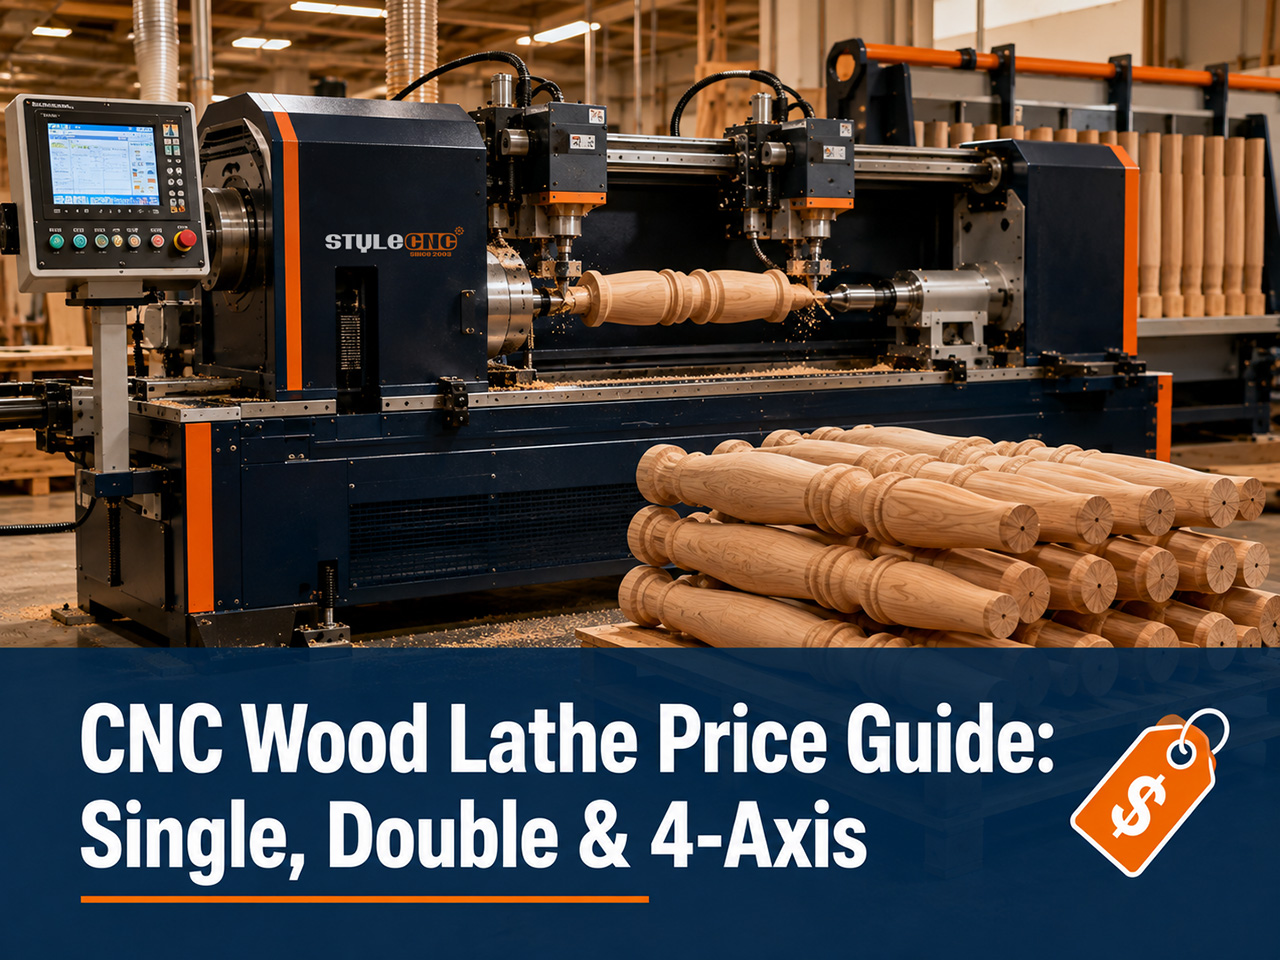
Strip away the branding and the price of a wood lathe is a short list of hardware decisions:
⦿ Axis count and blade sets: a 2nd axis with its own blades is the single largest price step, because it duplicates the cutting hardware.
⦿ Bed capacity: maximum length between centers and swing diameter scale the castings, rails, and ball screws with them.
⦿ The carving spindle: a router motor, its axis, and the control channel to run it add both hardware and software cost.
⦿ Automation: auto-feeding magazines and unload systems price separately and matter more than any spec at volume.
⦿ Build quality tier: cast iron beds, branded ball screws, and precision rails cost more than the alternatives and hold accuracy years longer.
The control system rides on top of all of it. Production wood lathes typically run DSP handle controllers that work offline from a USB stick, which keeps the machine simple to operate and cheap to support. Machines aimed at carved work carry fuller CNC controllers with profile software included, and the software maturity is worth weighing as part of the price: a controller that turns a drawn outline into a finished program in minutes saves operator hours every single week of ownership.
Reading a quote against this list turns a mystery price into an itemized one. When 2 machines sit $2,000 apart, the difference is nearly always visible in the axis count, the bed spec, or the rail and screw brands, and comparing models line by line in the chitsogozo chogulira lathe yoyenera ya CNC matabwa shows exactly how the configurations ladder up.
Price Bands by Configuration
The bands below reflect current pricing across the CNC wood lathe range, from bench machines to full-size production models:
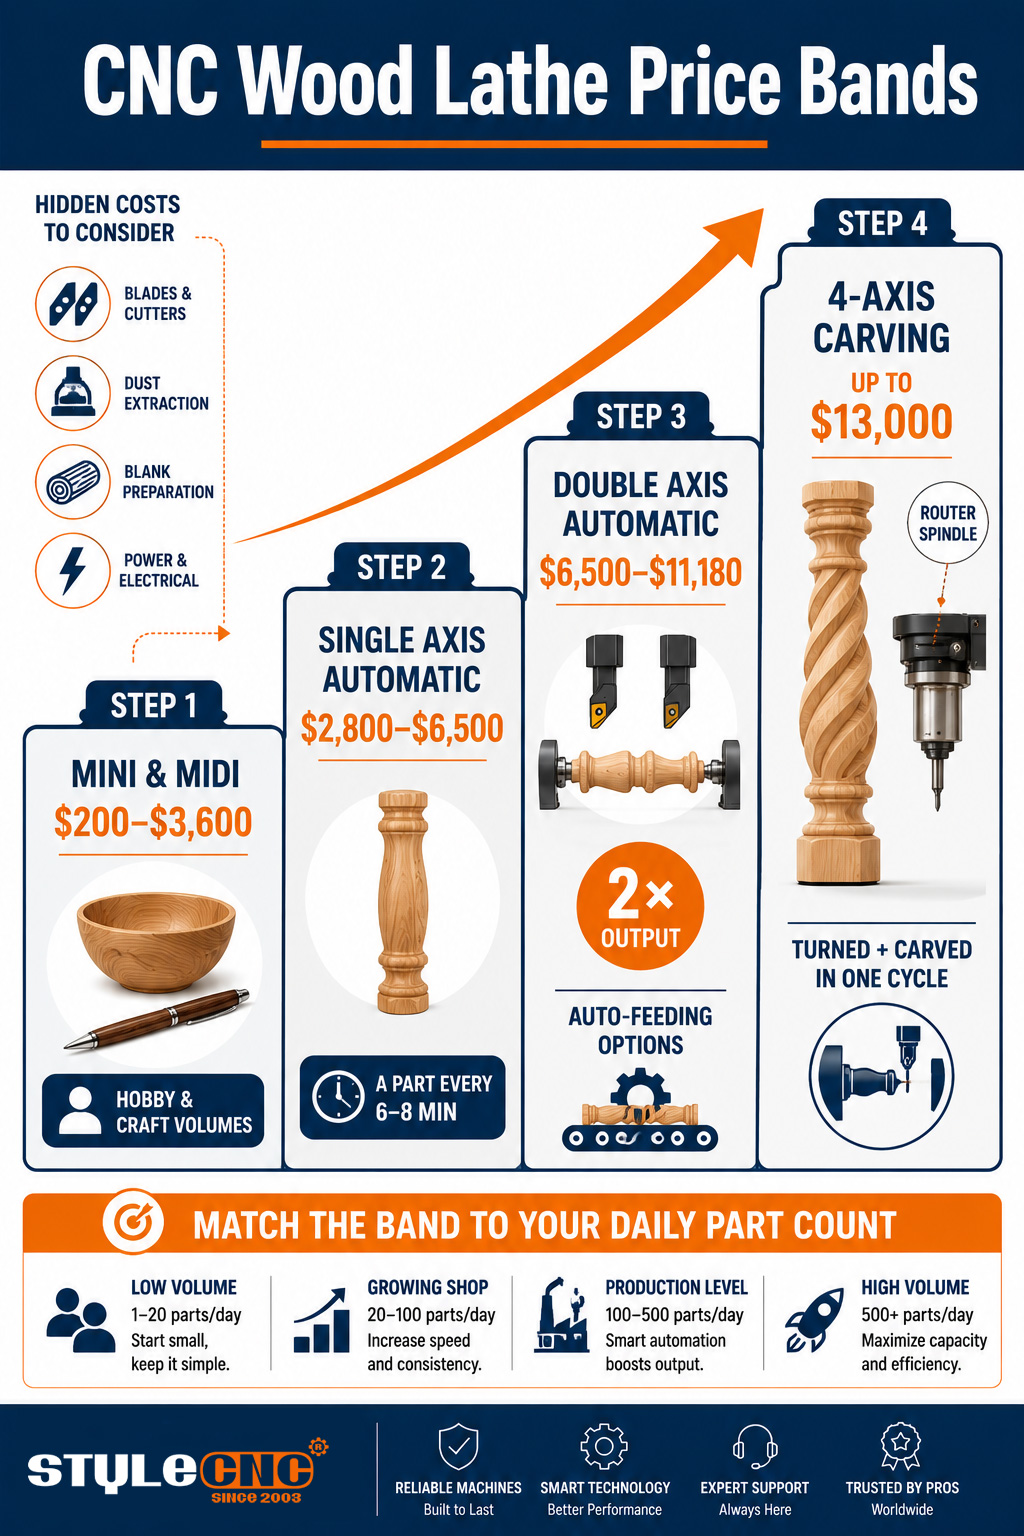
| Kalasi ya Makina | Mtengo Band | Zimene Mumapeza | Zotulutsa Zodziwika | Kuyeza |
|---|---|---|---|---|
| Mini and midi lathes | $ 200 ku $3, 600 | Bench machines for bowls, pens, small spindles; hand or light CNC control | Hobby and craft volumes | Largest part that fits between centers |
| Chozungulira chimodzi chokha | $ 2,800 ku $6, 500 | One tool carriage, double blades, cast iron bed, DSP control | A leg or bat every 6 to 8 minutes | Cycle time on your longest profile |
| Double axis automatic | $ 6,500 ku $11,180 | 2 blade sets cutting simultaneously, auto feeding options | Roughly double single axis output | Parts per shift at your diameters |
| 4-axis yokhala ndi spindle yosema | mpaka $13,000 | Rotary axis plus router spindle for flutes, spirals, carving | Turned and carved in one cycle | Share of catalog needing carved detail |
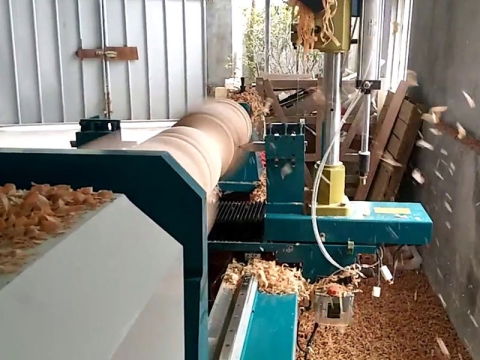
The middle bands do the interesting work. A single axis automatic already replaces template turning outright, producing a part every 6 to 8 minutes unattended within the cycle. The double axis step roughly doubles that output without doubling floor space or labor, which is why it dominates production spindle work from table legs to baseball bats. The comparison holds across the market too; independent roundups like the 10 best wood lathes compared consistently place the double axis class at the value peak for commercial turning.
Costs Beyond the Invoice
Owners meet 4 cost lines the quote never mentions:
⦿ Blades and cutters: profile blades are consumables, and hardwood volume wears them on a schedule you should budget, not discover.
⦿ Dust and chip handling: a production lathe generates shavings by the barrel, and extraction sized too small buries the rails by mid-shift.
⦿ Blank preparation: the lathe wants square, consistent blanks, which means saw capacity and stock handling upstream of the machine.
⦿ Power and air: check the spindle and feeder requirements against your supply before delivery day rather than after.
New vs Used: The Controller Decides
Used production lathes surface constantly, often at half the new price, and the mechanical parts are usually the safe half of the bet. Cast iron beds outlive owners. The risk concentrates in the controller: an orphaned control system with no parts, no documentation, and no one answering the phone turns a bargain into a static display the 1st time a board fails.
The practical test is support, not condition. A used machine on a current, supported controller with local technicians is a defensible buy; the same iron on a dead controller is not, whatever the price. Owner accounts in the ndemanga za makasitomala a lathe yamatabwa are worth reading in exactly this light, since they report which support experiences actually followed the sale.
If a used machine passes the controller test, inspect it the only way that means anything: under power, cutting your own blank. Watch the finished profile for ripple that signals worn centers or loose gibs, listen to the feed at full traverse, and run the same file twice to compare parts. Ten minutes of cutting reveals more than an hour of walking around the machine, and a seller who declines the demonstration has answered the question already.
Payback Math from Parts per Day
The economics reduce to a comparison every furniture shop can run in an afternoon. A skilled turner produces a plain leg in perhaps ten minutes and a carved profile far slower, at a skilled wage and with the day's variance built in. A single axis machine holds 6 to 8 minutes per part all shift; a double axis holds close to half that.
Worked simply: at 60 legs a day, a double axis machine saves several turner-hours daily, and against a mid-band price near $8,000 the capital typically returns inside the 1st year of steady production. At 15 legs a day the same machine idles most of the shift, and the mini or single axis band serves better. The volume decides the band, and pretending otherwise only defers the decision to the accountant.
Carved work runs the same math with a heavier thumb on the scale, because hand carvers are scarcer than turners and their hours cost more. A 4-axis machine producing fluted legs in one cycle is not competing against a fast worker; it is competing against work the shop currently declines or outsources. When the payback calculation includes orders you could not previously accept, the carving band often clears its premium faster than the plain-turning bands clear theirs.
Matching the Band to Your Catalog
Walk the elimination downward. If your work is bowls, pens, and short craft spindles at hobby volume, the mini and midi band covers it and everything above is idle capacity. If you turn plain profiles in production quantity, the single axis automatic is the entry point and the double axis is the volume play. If the catalog includes fluted, twisted, or carved work, only the 4-axis carving band produces it in one cycle, and the premium buys back the 2nd machine and 2nd setup the work would otherwise need. The parts themselves settle the question, and browsing the Chithunzi cha polojekiti yopangira lathe yopangira matabwa ya CNC against your own product photos is the fastest way to see which band your catalog actually lives in.
2 catalog patterns deserve a named mention because they anchor so many purchases. Staircase shops sizing for newel posts and balusters should let the longest post set the bed length and buy the double axis for the baluster count, since a staircase order arrives as dozens of matching parts on a deadline. Bat makers face the opposite shape: one slender tapered profile at volume, where the thin handle rewards the double axis machines whose twin supports tame the chatter that plagues single-point turning on flexible stock. Naming your own pattern this concretely is most of the buying decision.
Common Mistakes When Buying on Price
❎ Comparing prices without comparing axis counts, then wondering why the cheaper machine turns half as fast.
❎ Buying hobby-band capacity for production ambitions and outgrowing it in months.
❎ Paying the carving premium for a catalog of plain round profiles.
❎ Ignoring the controller ecosystem on a used machine because the iron looked good.
❎ Leaving blades, extraction, and blank preparation out of the first-year budget.
Buyer Checklist Before You Quote
✅ Count your honest daily part volume across a normal month.
✅ List maximum part length and diameter, and add margin before matching bed specs.
✅ Split your catalog into plain turned versus carved, and let the carved share justify or kill the 4-axis premium.
✅ Price the double axis step against the turner-hours it saves at your wage rates.
✅ Confirm controller support, parts, and training for your region before comparing final prices.
Get a Quote Matched to Your Band
Compare single, double, and 4-axis configurations with current pricing across the full range of Makina opukutira ndi matabwa a CNC otembenuzira ndi kusema, and get a free quote sized to your parts, volumes, and budget.